Using abrasive flow machining, Extrude Hone AFM can polish difficult internal geometry by directing abrasive-filled polymer media through or across the functional flow path.
Why Internal Surface Finish Matters
A centrifugal pump works by moving fluid through an impeller and housing.
Roughness along those surfaces can create drag.
Manufacturing methods may leave raised material, casting texture, machining marks, or other irregularities.
Extrude Hone AFM notes that poor surface finish can slow the volume of fluid pumped through a system. Improving the impeller, turbine, and housing can support better efficiency and reduced motor stress.How AFM Improves the Flow Path
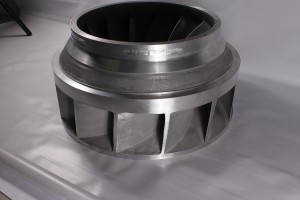 Abrasive flow machining uses a viscoelastic carrier filled with abrasive particles.
The media is pushed through the workpiece hydraulically.
It conforms to blade surfaces, curves, and passage restrictions.
As it travels, abrasive particles remove positive surface features.
AFM may provide:
- Impeller polishing
- Turbine finishing
- Pump-housing improvement
- Blade-surface smoothing
- Internal deburring
- Passage polishing
- Flow-path geometry refinement
Nashville Industrial and Manufacturing Applications
Middle Tennessee supports automotive manufacturing, industrial equipment, food and beverage production, healthcare manufacturing, transportation, and advanced manufacturing.
Pumps are used throughout these industries for process fluids, water, cooling, lubricants, fuels, and other applications.
Turbines and impeller-type components may also appear in aerospace, industrial, and power-related systems.
AFM offers a specialized finishing option when those internal surfaces cannot be polished efficiently using ordinary tools.
Reaching Between Blades
Impellers present a difficult combination of narrow spacing and curved geometry.
Extrude Hone AFM specifically highlights its ability to improve surface finish and remove material from restricted areas between blades.The flexible media follows the internal shape instead of requiring a rigid tool to fit into every space.
This can help produce more uniform treatment across the flow surface.
Flow Geometry and Restriction
The abrasive process naturally becomes more active in restrictive regions.
As a passage narrows, media velocity and pressure increase, resulting in greater local material removal.
This characteristic can be useful when raised features or restrictive regions interfere with the intended flow path.
Extrude Hone AFM uses tooling and process controls to focus this effect appropriately.Tooling Protects Non-Target Areas
AFM tooling holds and supports the workpiece, directs abrasive media to the surface requiring treatment, and protects areas where abrasive flow is not desired.
This allows selected pump or turbine features to be processed without treating every surface identically.
Surface Finish Targets
Extrude Hone AFM publishes representative finish improvements such as approximately:- 16–8 Ra to 3–4 Ra
- 32 Ra to 8 Ra or better
- 64 Ra to 16 Ra or better
Actual results depend on geometry and material.
Production Repeatability
Once a process is established, Extrude Hone AFM can monitor surface-finish improvement and stock removal for consistent treatment of repeat components.
This may be valuable for OEM suppliers and other manufacturers producing recurring pump or turbine parts.
Request Nashville Turbine and Pump Finishing
Call (562) 531-2976 to discuss turbine and pump flow finishing for Nashville, TN with Extrude Hone AFM.
FAQs
Can AFM polish industrial pump components?
Yes. Suitable impellers, housings, and internal flow features can be evaluated.
Can AFM remove burrs during polishing?
Yes. Abrasive flow machining can combine surface polishing with internal deburring where required.
Does Extrude Hone AFM serve Nashville manufacturers?
Yes. Extrude Hone AFM serves manufacturers nationwide.